Compound range pressure gauges are designed to measure both positive and negative pressures within a single instrument, making them ideal for applications where vacuum and pressure conditions exist. These gauges offer cost savings and process efficiency benefits over using separate gauges for positive and negative pressure measurement.
 DS200P Sanitary Low Range Pressure Gauge, Switch and Sensor - All in one electronic switch, gauge and sensor designed specifically for use in the food, drink and biomedical industry for measuring process pressures.
 DS200 Combined Pressure Switch, Gauge and Sensor - Three in one electronic pressure switch, digital pressure gauge and pressure sensor with pressure ranges from 100 mbar up to 600 bar (1.5 to 9000 psi).
 ADT681 Digital Pressure Gauge - The ADT681 digital pressure gauge family covers a wide range of pressures from as low as 1 inH20 differential to as high as 36,000 psi gauge.
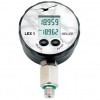 LEX1 (Ei) High Accuracy Digital Pressure Gauge - High precision digital pressure gauge with an accuracy of 0.05% full scale in pressure ranges from 0...30 mbar up to 0...1000 bar.
- +/- 2.5 mbar (1 inH2O) DP Pressure Gauge
- Hastelloy diaphragm -100 to 50 kPa g range manometer
- -0.1 to +0.1 inH2O g range 4-20mA signal air pressure sensor and display for pharmaceutical manufacturing use
Send us your enquiry to discuss your Compound Range Pressure Gauges application with a product specialist, and they will help you select the best option to suit your specific requirements.
Compound range pressure gauges are essential tools for measuring pressure in systems that fluctuate between positive and negative values. These gauges are calibrated to display both vacuum and pressure readings on a single display, providing a comprehensive view of the system’s pressure status. This dual-measurement capability eliminates the need for separate gauges, simplifying installation and reducing costs.
Product Advantages
Compound range pressure gauges offer significant operational, financial, and mechanical advantages in industrial pressure measurement systems. By integrating bi-directional sensing capabilities into a single device, these instruments streamline process monitoring, reduce hardware complexity, and eliminate common vulnerabilities associated with single-range pressure instrumentation in dynamic vacuum-to-positive pressure environments.
Cost-Effectiveness
Combining positive gauge and vacuum measurement capabilities into a single unit significantly reduces upfront capital expenditure by eliminating the need to purchase two separate instruments. Beyond initial equipment procurement, it lowers ongoing operational expenses by reducing inventory holding costs, reducing calibration and certification requirements, and cutting down on redundant spare parts stock across facility maintenance operations.
Space Optimization
Integrating dual-range sensing into one housing minimizes physical footprint requirements on control panels, manifold blocks, and process piping. This space efficiency simplifies equipment layout design in compact OEM machinery, skid packages, and crowded process lines where mounting real estate is constrained.
Simplified Installation
Installing a single compound gauge requires only one process connection tap, isolation valve, and mounting bracket. This reduces total pipework engineering, cuts down on installation labor hours, and directly decreases the number of mechanical joints and potential leak paths within high-purity or critical process systems.
Reduced Maintenance
Fewer installed instruments directly translate to decreased maintenance overhead and inspection cycles. With half the total number of pressure connections, gaskets, and sensing elements, facility teams spend less time troubleshooting leaks, conducting routine visual checks, and re-calibrating instruments.
Overload Protection
Standard dedicated vacuum gauges are highly susceptible to mechanical damage, calibration drift, or diaphragm rupture if exposed to positive pressure cycles. A compound gauge utilizes a sensing element designed and calibrated to smoothly transition across the zero point and handle positive pressure limits, preventing sensor failure without requiring complex external overpressure protection valves or snubber systems.
Product Applications
Compound range pressure gauges are critically deployed across a broad spectrum of industrial, chemical, and pharmaceutical manufacturing processes that depend on dynamic pressure transitions. In systems that routinely cycle between initial vacuum evacuation and subsequent positive pressure pressurization—such as thermal separation, moisture extraction, vapor sterilization, vessel loading, reaction monitoring, and differential filtration—these bi-directional gauges provide continuous, real-time visual and electronic feedback. By seamlessly monitoring both sub-atmospheric and positive gauge pressure realms within a single instrument, compound gauges ensure process integrity, optimize operational efficiency, prevent cross-contamination, and protect equipment from unexpected pressure fluctuations across complex industrial workflows.
Distillation
Distillation processes, particularly vacuum distillation of heat-sensitive compounds, often begin with a deep vacuum phase to lower the boiling point of the substance being purified. Once the desired sub-atmospheric vacuum level is established, thermal energy is introduced to initiate boiling, causing vapors to generate rapidly. As volatile components vaporize and migrate toward condensation columns, internal vessel pressure can transition from deep vacuum into positive pressure. A compound range pressure gauge continuously tracks this full spectrum—monitoring the initial vacuum pulled by vacuum pumps and tracking subsequent positive vapor pressures—ensuring precise temperature-pressure relationships, preventing thermal degradation of volatile substances, and maintaining stable vapor flow throughout the distillation sequence.
Drying
Industrial drying operations, including freeze-drying (lyophilization) and vacuum oven processing, rely on controlled pressure cycles to extract moisture efficiently without damaging heat-sensitive product matrixes. Initially, an intense vacuum phase is induced to reduce moisture vapor pressure and promote rapid sublimation or evaporation at low ambient temperatures. Subsequently, dry purge gas or inert blanket media is introduced under positive gauge pressure to sweep out residual vapor, break the vacuum seal, or facilitate pneumatic discharge. Compound range gauges effectively track these wide multi-bar pressure swings, enabling operators to optimize process cycle times, verify complete moisture removal, and prevent structural collapse or degradation of dried products.
Sterilization
Sterilization protocols in pharmaceutical manufacturing and clinical autoclaves depend on alternating vacuum conditioning and steam pressurization pulses. During pre-vacuum phases, deep vacuum pulses evacuate trapped air pockets from intricate equipment, porous loads, and vessel interiors. Following air removal, saturated steam or gaseous sterilants are injected under high positive pressure to ensure complete thermal penetration and microbicidal efficacy. Compound range pressure gauges accurately monitor both the pre-vacuum depth and high-pressure sterilization dwell times, ensuring compliance with strict regulatory validation standards, preventing air entrapment, and confirming safe vessel depressurization prior to door release.
Evacuation and Filling
Industrial processes involving the evacuation and filling of storage tanks, gas cylinders, aerosol containers, and food/beverage packaging require strict pressure control across both negative and positive regimes. Containers are first evacuated under vacuum to eliminate ambient atmospheric oxygen, moisture, and potential contaminants. Once a verified vacuum seal is achieved, liquid products, propellants, or protective inert cover gases are charged under positive pressure. Compound range gauges monitor both the evacuation vacuum limit and the precise positive final fill pressure, guarding against container implosion during vacuum pulling, over-pressurization during filling, and product oxidation during long-term storage.
Chemical Reactors
Batch chemical reactors and synthesis vessels frequently undergo dynamic pressure changes caused by raw material charging, degassing, exothermic reactions, and inert gas blanketing. Reactors may initially be evacuated under vacuum to pull liquid reagents into the vessel or remove dissolved oxygen that could cause unwanted side reactions. As the reaction proceeds, gaseous byproducts or thermal expansion can raise internal pressure significantly above atmosphere. Installing a compound range pressure gauge provides continuous visibility across negative and positive regimes, allowing process engineers to manage reaction rates, prevent runaway over-pressurization, and execute safe inert gas purges.
Filtration and Membrane Separation
Industrial filtration assemblies, cross-flow membrane systems, and vacuum-assisted dewatering units utilize differential pressure to drive liquid-solid separation across filter media. Depending on system configuration and process stage, filtration forces may be generated by suction vacuum pulled downstream of the filter bed or positive feed pressure applied upstream. Furthermore, filter cake backwashing cycles involve reversing pressure direction. Compound range gauges allow operators to monitor differential pressures across both vacuum pull and positive pressure wash phases, enabling precise detection of filter clogging, membrane fouling, and optimal cake release timing.
Product Selection
Selecting the appropriate compound range pressure gauge requires careful evaluation of system operating conditions, fluid characteristics, and performance requirements. To ensure safe, accurate, and long-lasting operation, key selection criteria must be systematically assessed, including operating pressure ranges, chemical compatibility of wetted parts, overpressure capabilities, required measurement precision, and instrument output or display preferences.
Pressure Range and Units
Determine the full dynamic span of the system, including maximum vacuum levels (e.g., -1 bar, -30 inHg) and peak positive operating pressures. The gauge’s working range should be specified so that normal operating pressures fall within the middle third of the full scale. Additionally, ensure the required engineering units (such as bar, psi, kPa, or inH2O) match system documentation and operator monitoring standards.
Media Compatibility and Wetted Materials
Evaluate the chemical composition, temperature, and physical state of the process media contacting the sensing element. Selecting appropriate wetted materials—such as 316L stainless steel, Hastelloy, or specialized sanitary diaphragms—prevents chemical corrosion, material degradation, and process contamination in harsh or high-purity applications.
Overpressure Protection Limits
Identify potential system pressure spikes, water hammer events, or accidental over-pressurization conditions. Choose an instrument with built-in overpressure protection limits that exceed the maximum conceivable system surge to prevent permanent calibration drift, diaphragm distortion, or internal mechanical failure.
Accuracy and Calibration Requirements
Specify the level of measurement precision required for process safety and quality control. General industrial applications may require standard dial gauge accuracy (e.g., ±1.0% to ±1.6%), while critical process monitoring or laboratory testing may necessitate high-accuracy digital gauges (e.g., ±0.05% full scale) with traceable calibration certificates.
Electrical and Display Output Options
Determine whether local visual indication is sufficient or if automated process integration is required. Options range from traditional mechanical dial faces to digital displays with configurable switch outputs, 4-20 mA analog transmitters, or digital communication protocols for seamless PLC and SCADA system connectivity.